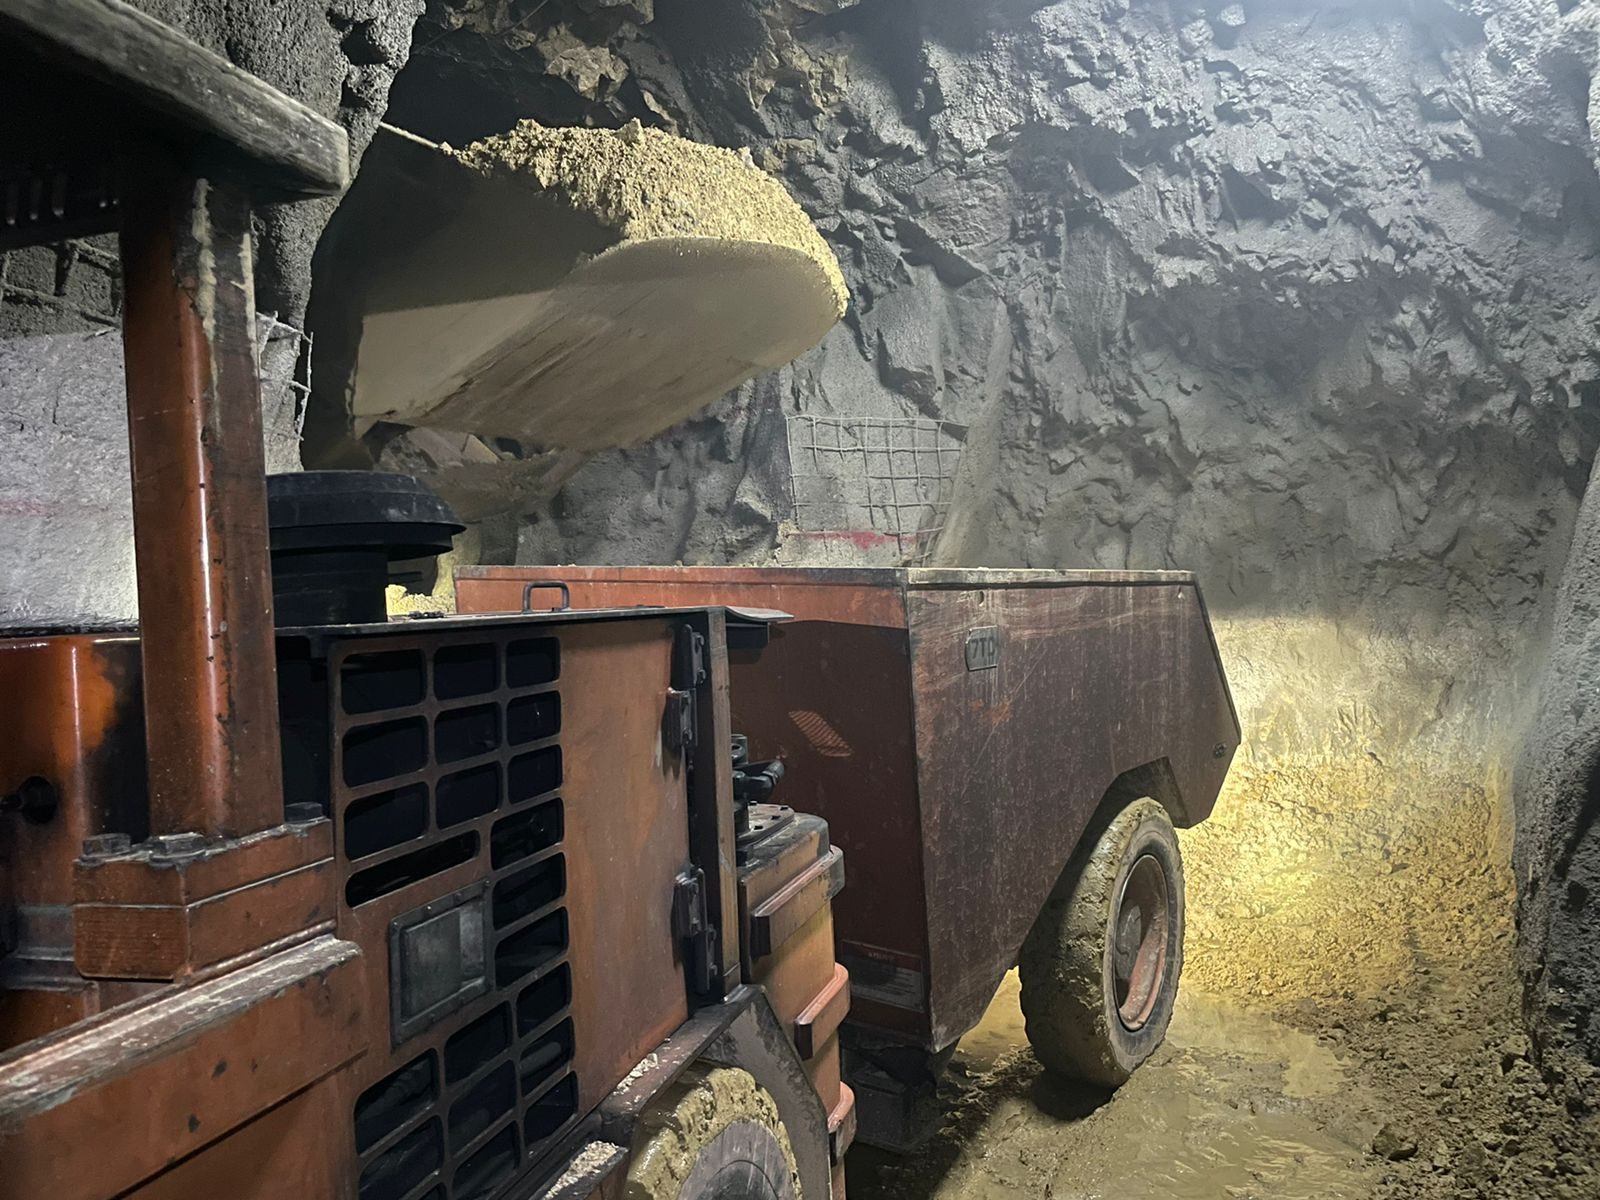
Mucking & hauling equipment
New mucking and hauling equipment brought into the mine.
Operations
With the new circuit designed, the company carried out a comprehensive revamp of both the mine and the plant at Mina Real.
Every upgrade, one by one
New mucking and hauling equipment brought into the mine.
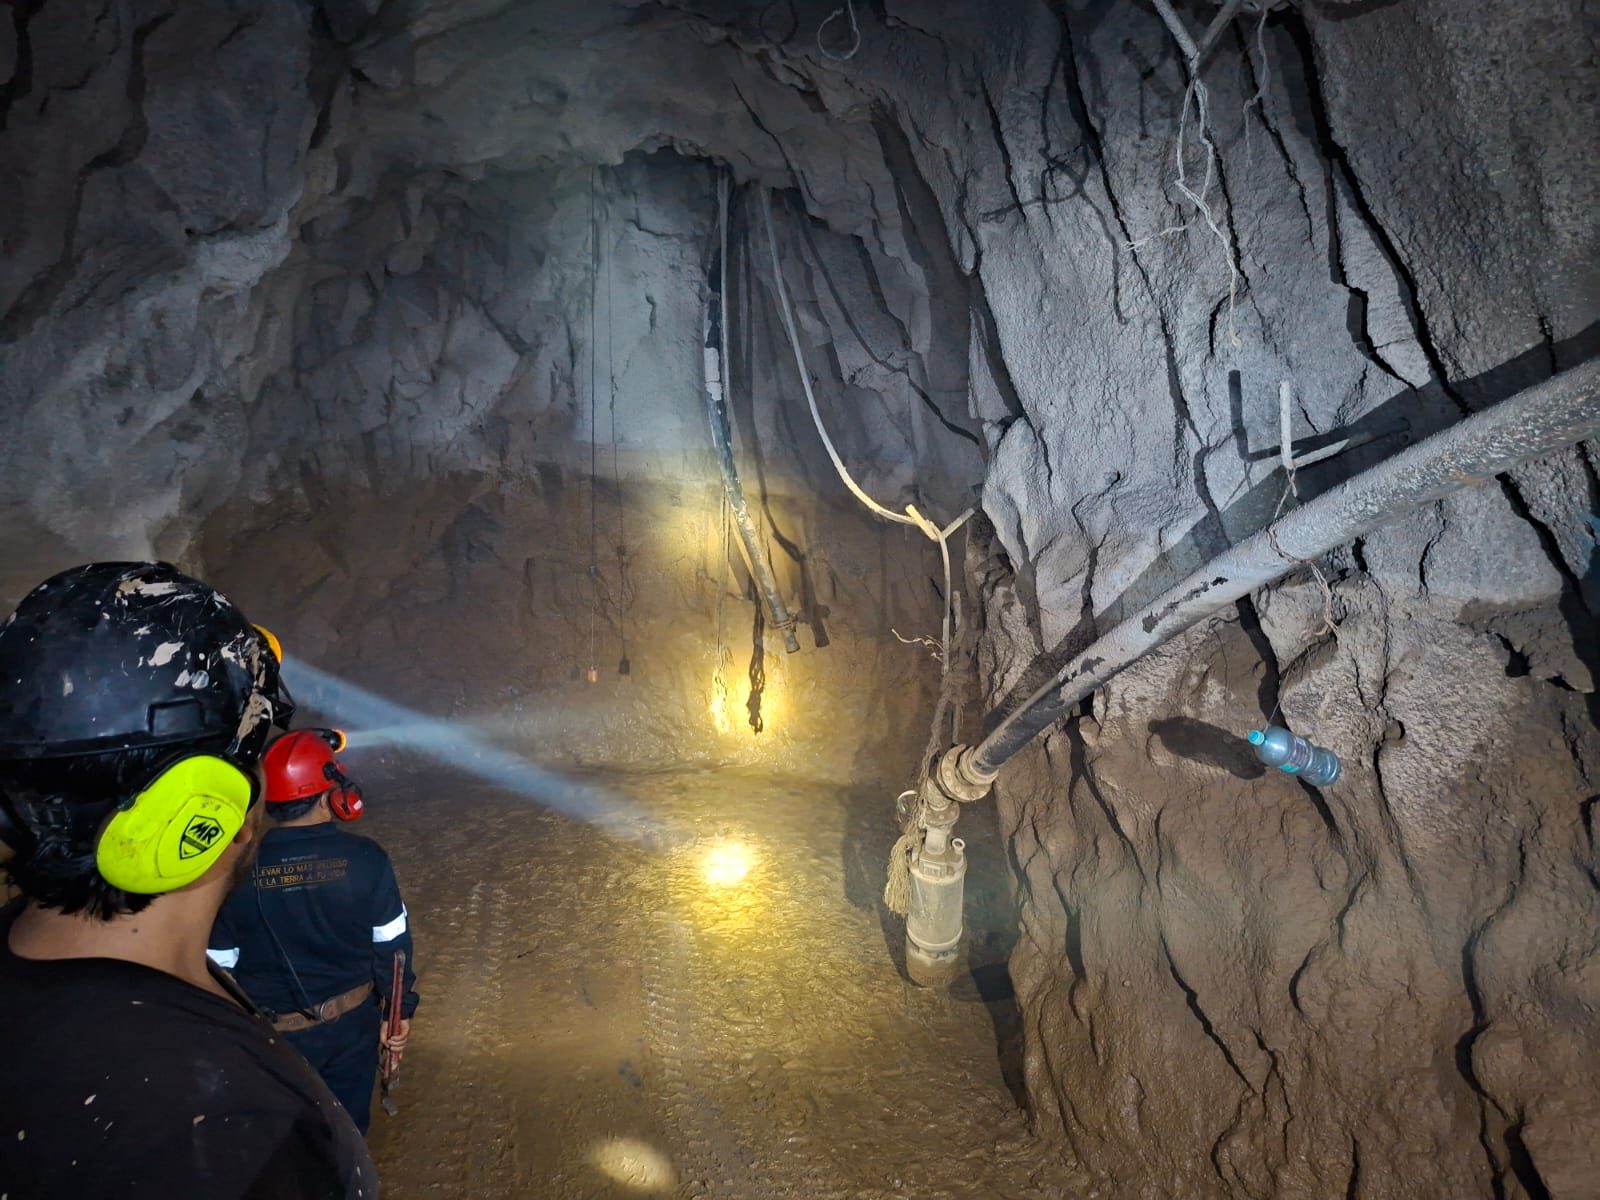
Mine water pumping stations rehabilitated, including cleaning of sump 018.
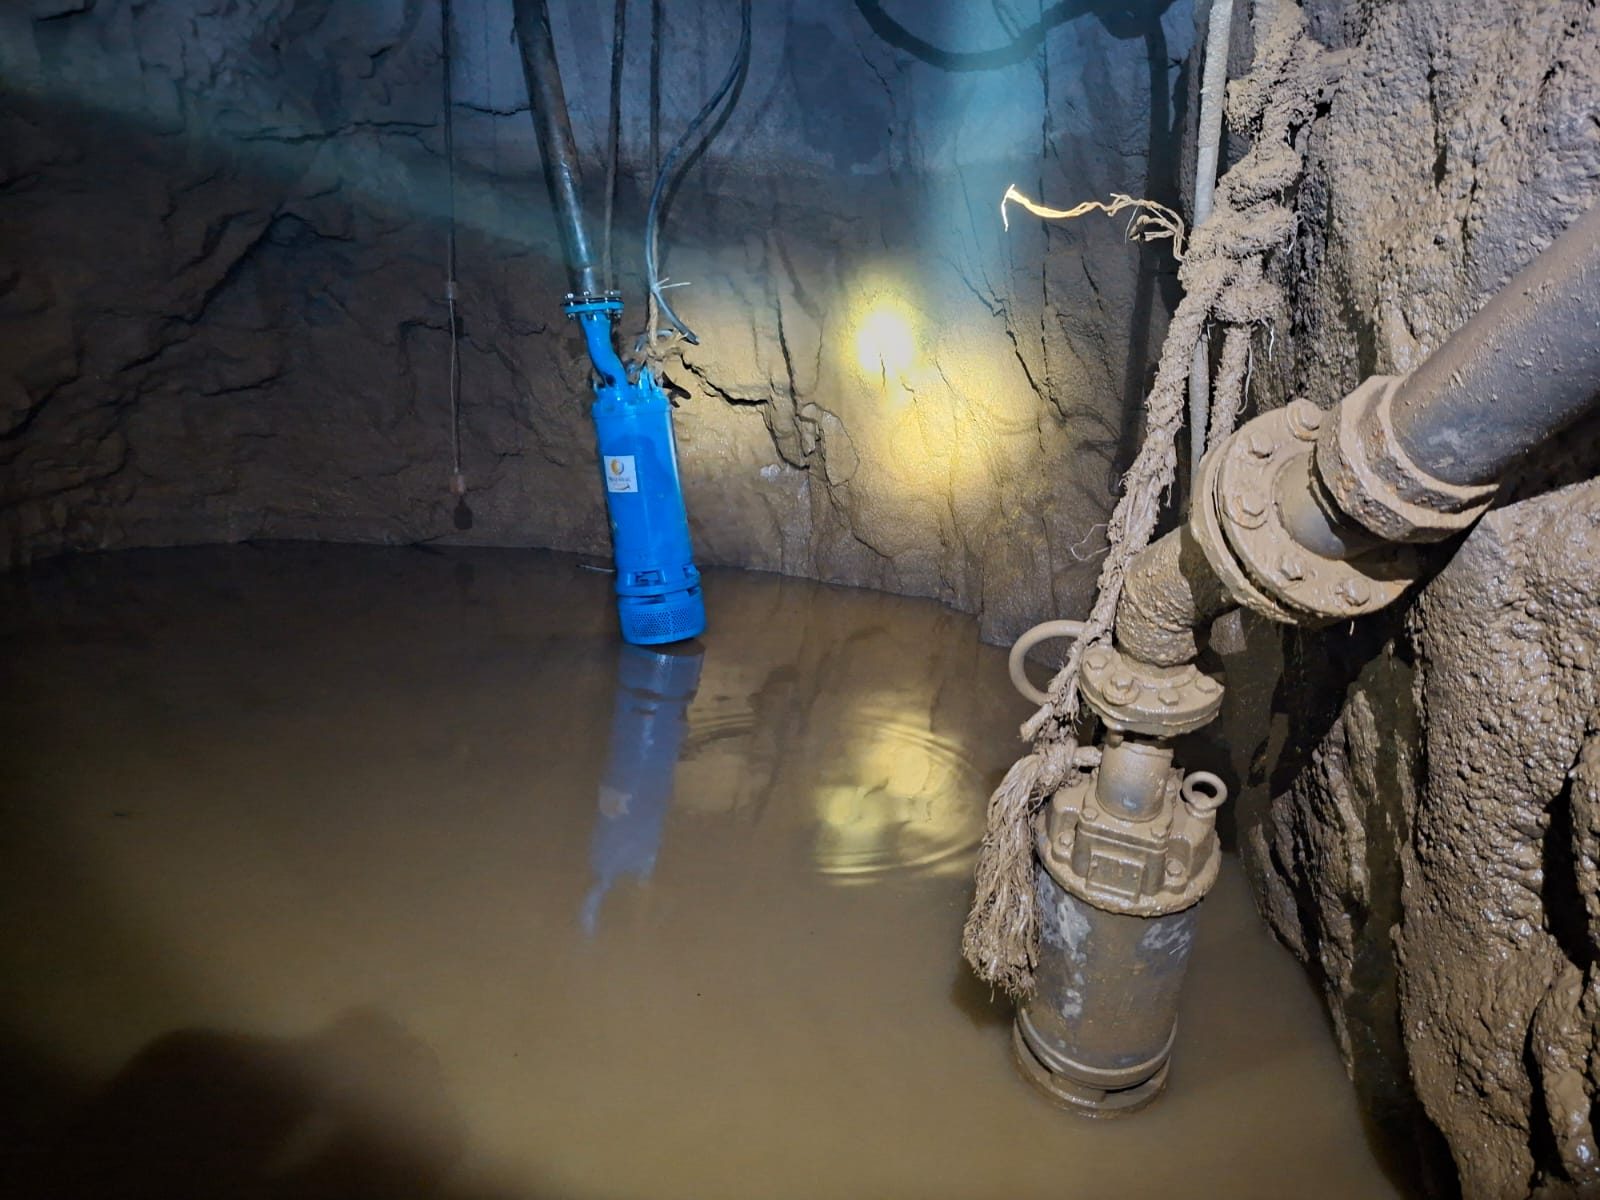
New pumps installed, including a 40 HP pump at sump 018.
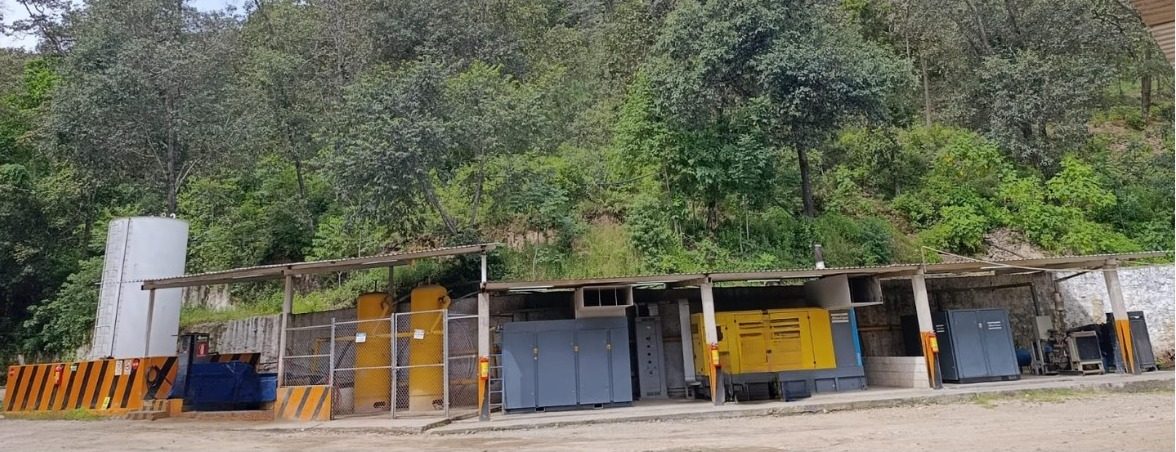
Mine electrical systems upgraded.
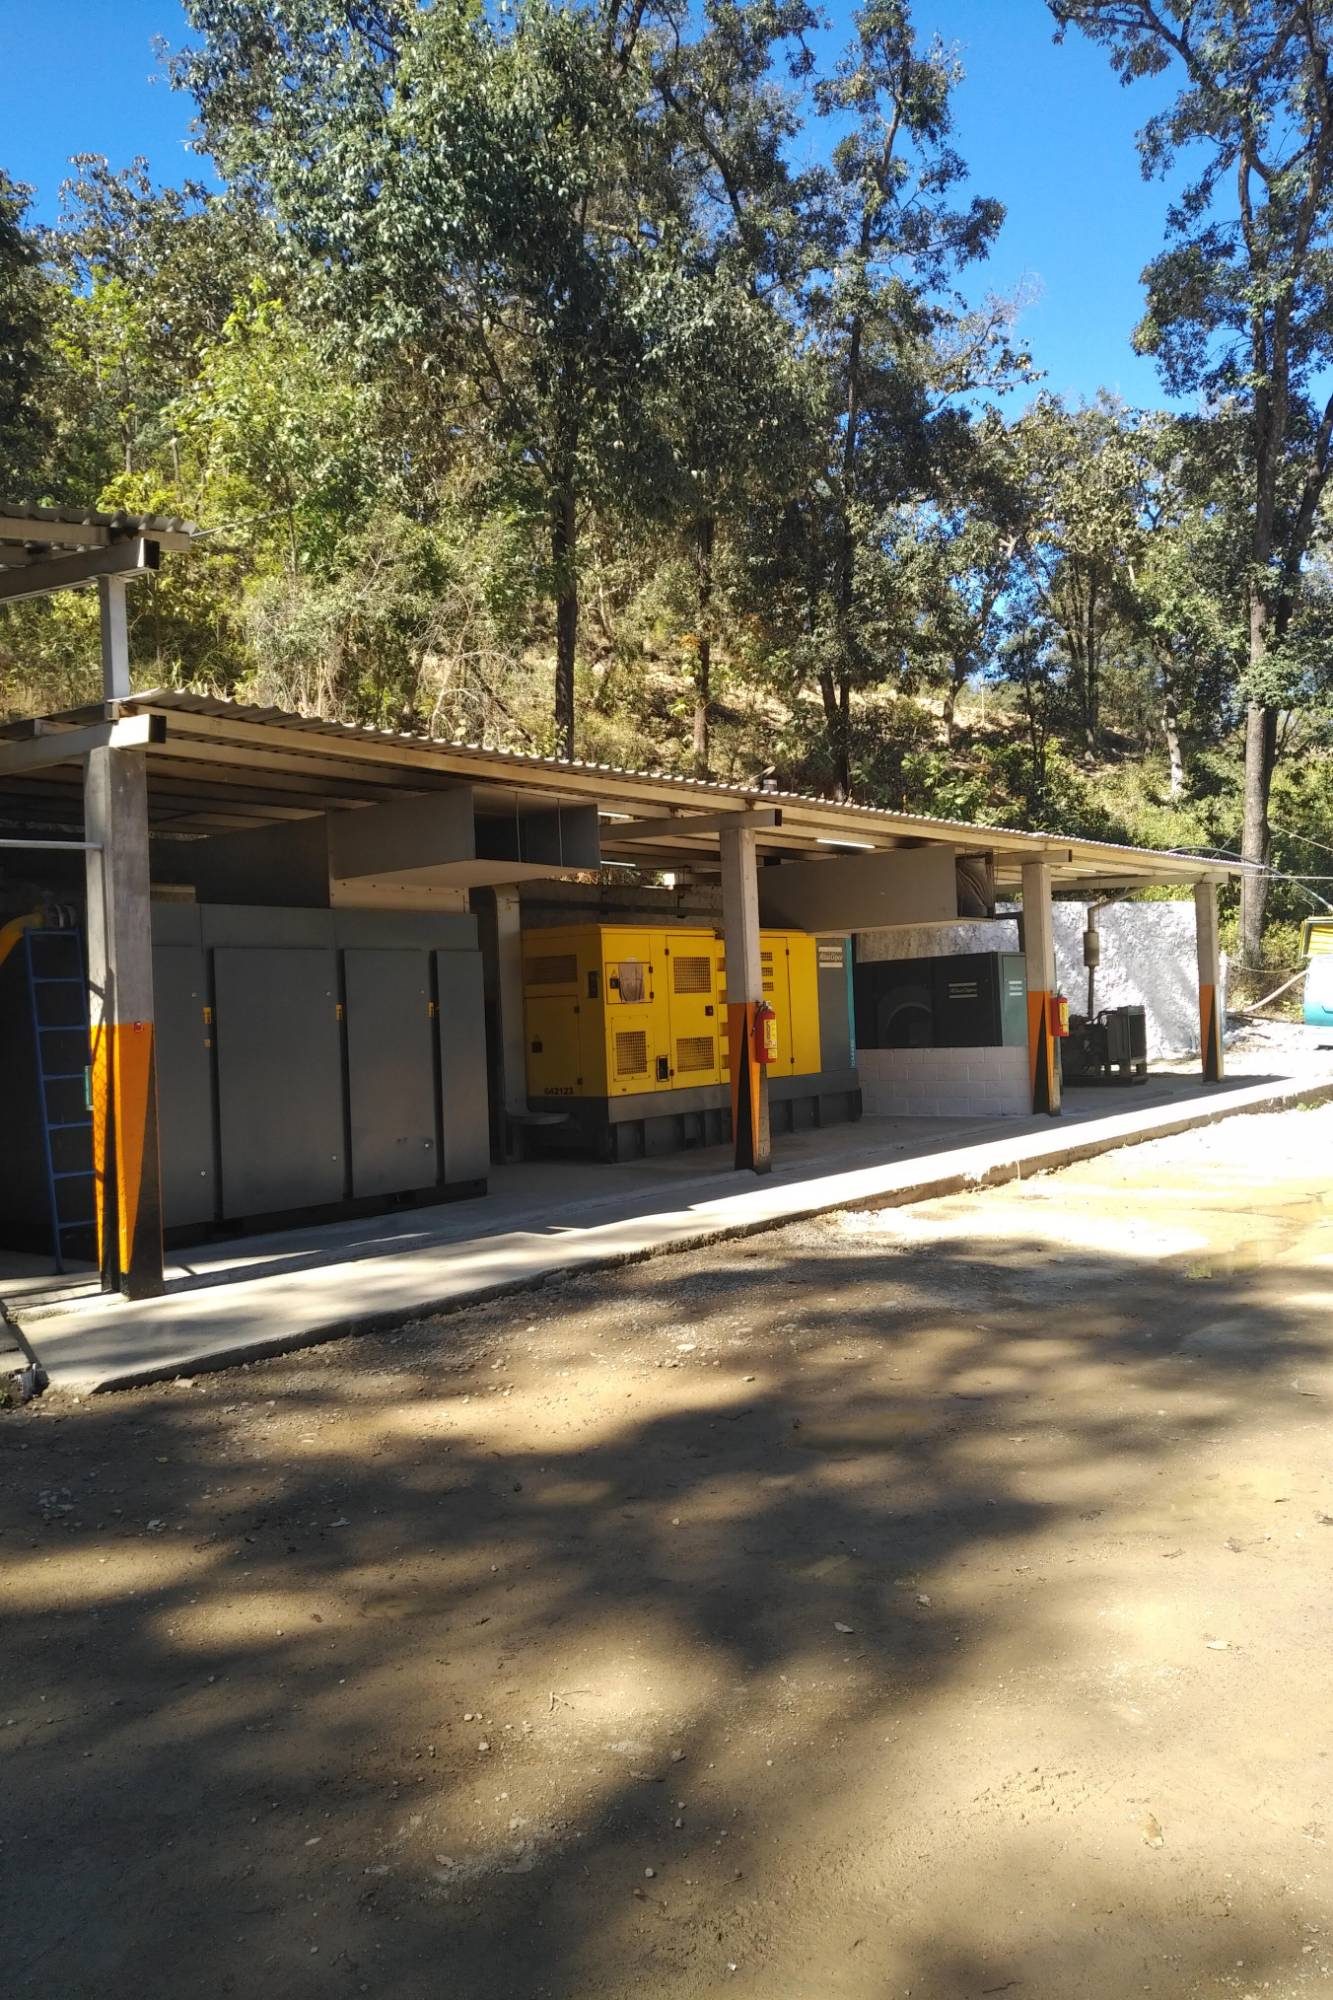
Mine compressed-air systems upgraded.
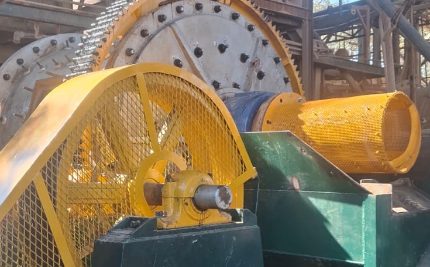
After the 6′ × 5′ mill went out of service in October 2025, the company sourced a used 6′ × 6′ mill, rebuilt and installed it, with a corresponding slurry pump upgrade. It was commissioned and began operating in late December 2025.
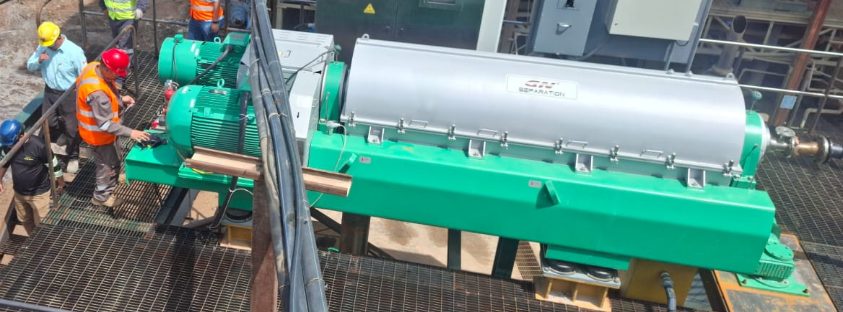
A high-speed centrifugal decanter for liquid-solid separation, installed and started up, recovers water, residual values and cyanide for reuse.
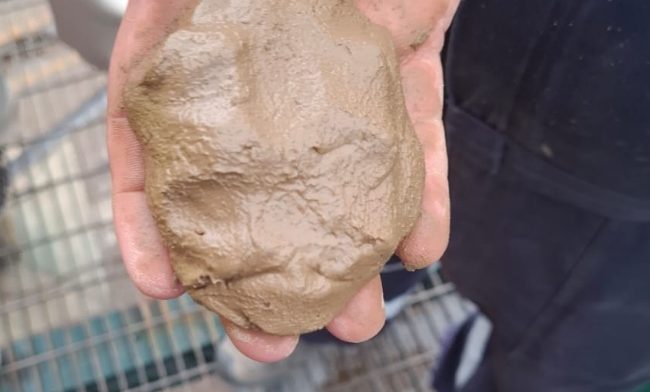
Water is recovered by the centrifugal decanter for reuse.
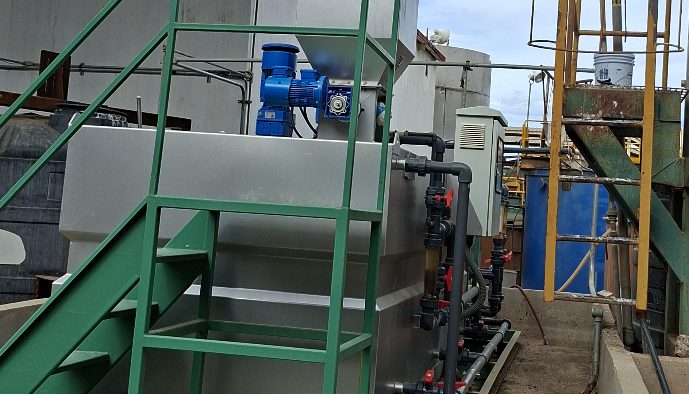
Cyanide is recovered for reuse, cutting fresh reagent consumption.
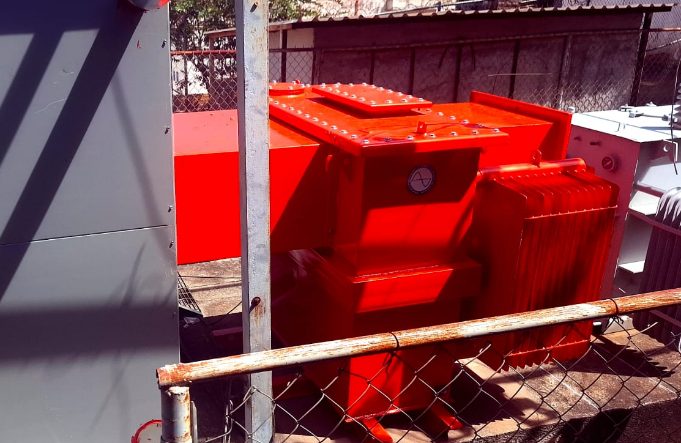
A new electrical substation, with a 750 kVA transformer and compact substation installed.
An expanded tailings filtering station, enabling dry-stacked tailings storage.
Tailings stored dry-stacked, rather than wet.
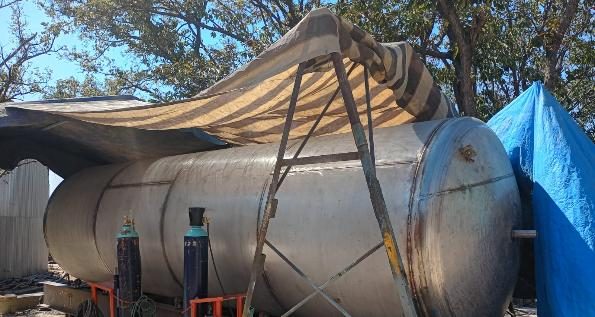
New stainless-steel process tanks, including two reagent tanks with stainless-steel piping and pumps, an acidity/basicity control tank, and a new 18,500-litre stainless-steel tank for ammonium bisulfite.
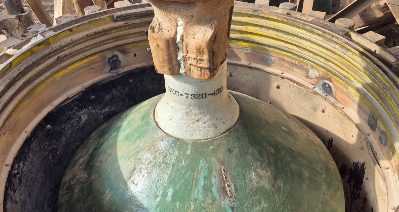
Primary, secondary and tertiary crushing circuits revamped, including repairs to the jaw crusher and the 4 ft and 3 ft cone crushers.
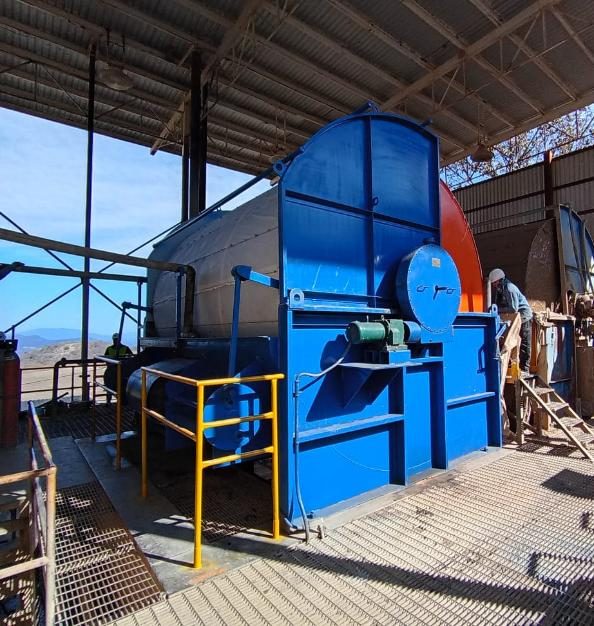
Existing drum filters fully rehabilitated. On vacuum filter no. 2, damaged steel was replaced, filter screens changed and the filter drive rebuilt.
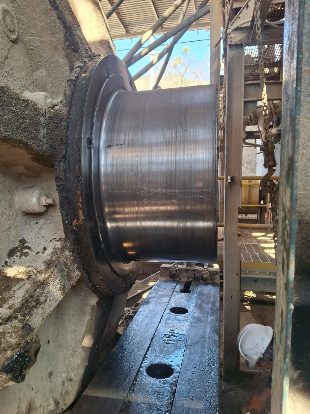
Babbitt bearing replaced on the 6′ × 12′ ball mill.
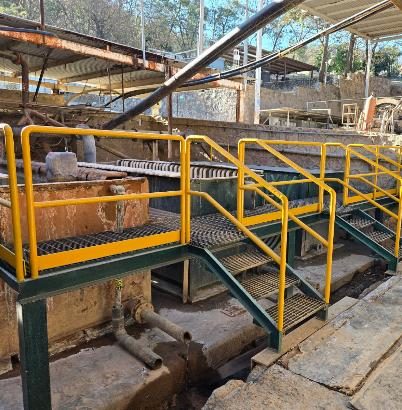
Two new Butters filters constructed for the precipitation circuit.
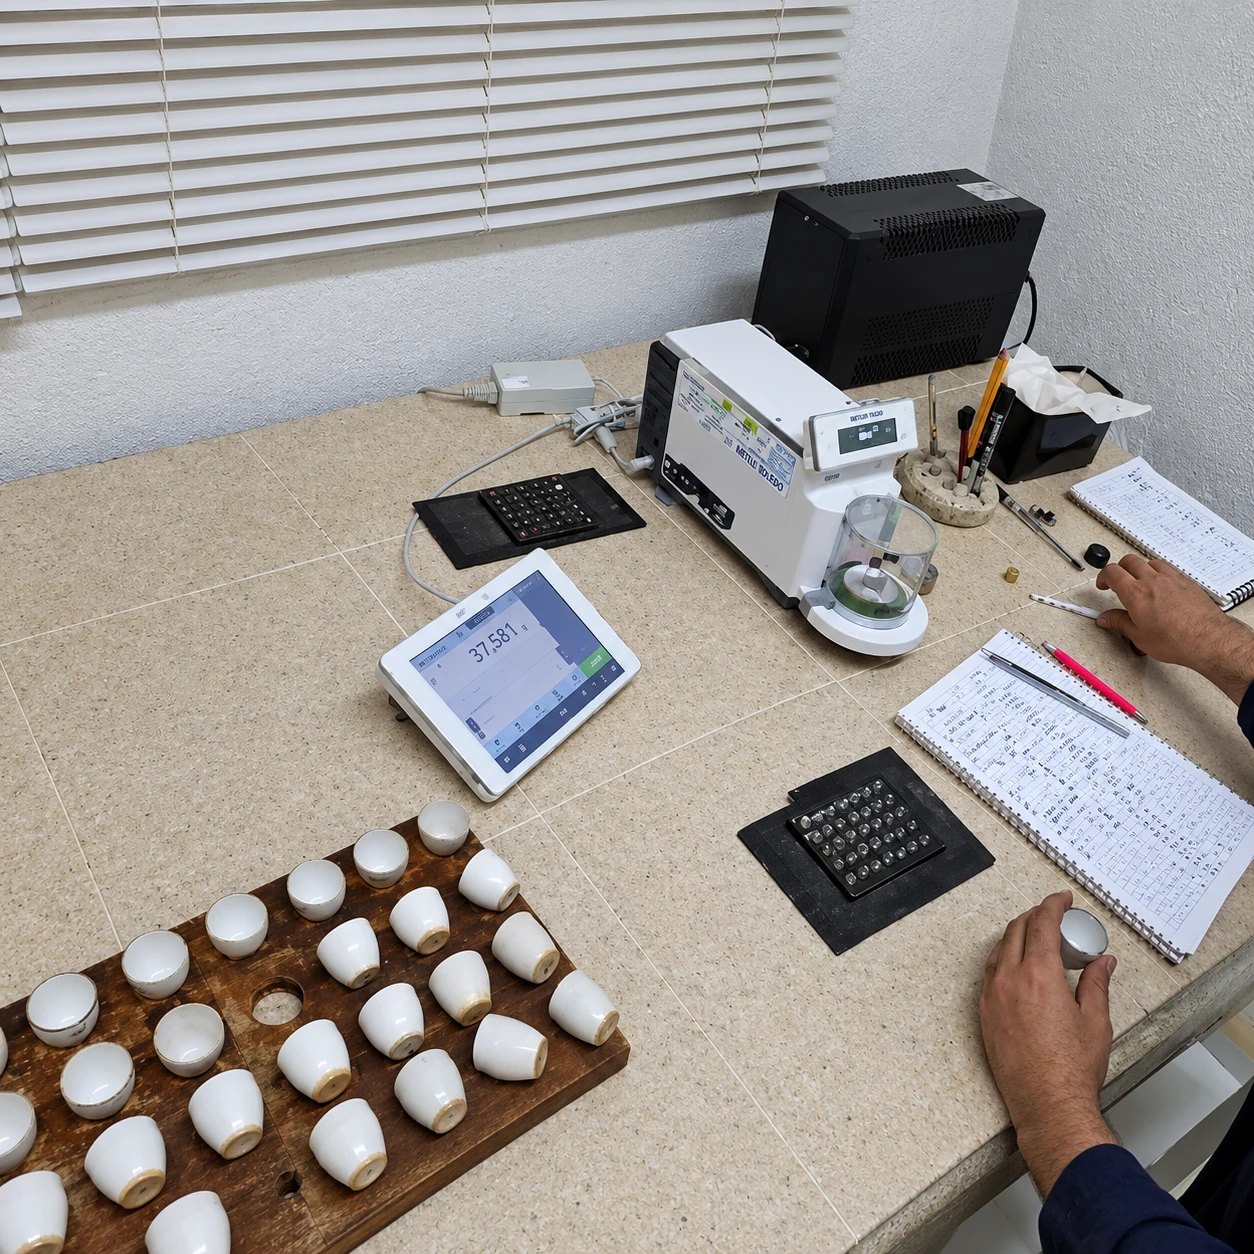
A micro-balance for weighing gold and silver installed and in operation.
New mucking and hauling equipment brought into the mine.
Mine water pumping stations rehabilitated, including cleaning of sump 018.
New pumps installed, including a 40 HP pump at sump 018.
Mine electrical systems upgraded.
Mine compressed-air systems upgraded.
After the 6′ × 5′ mill went out of service in October 2025, the company sourced a used 6′ × 6′ mill, rebuilt and installed it, with a corresponding slurry pump upgrade. It was commissioned and began operating in late December 2025.
A high-speed centrifugal decanter for liquid-solid separation, installed and started up, recovers water, residual values and cyanide for reuse.
Water is recovered by the centrifugal decanter for reuse.
Cyanide is recovered for reuse, cutting fresh reagent consumption.
A new electrical substation, with a 750 kVA transformer and compact substation installed.
An expanded tailings filtering station, enabling dry-stacked tailings storage.
Tailings stored dry-stacked, rather than wet.
New stainless-steel process tanks, including two reagent tanks with stainless-steel piping and pumps, an acidity/basicity control tank, and a new 18,500-litre stainless-steel tank for ammonium bisulfite.
Primary, secondary and tertiary crushing circuits revamped, including repairs to the jaw crusher and the 4 ft and 3 ft cone crushers.
Existing drum filters fully rehabilitated. On vacuum filter no. 2, damaged steel was replaced, filter screens changed and the filter drive rebuilt.
Babbitt bearing replaced on the 6′ × 12′ ball mill.
Two new Butters filters constructed for the precipitation circuit.
A micro-balance for weighing gold and silver installed and in operation.
01Mine
New mucking and hauling equipment was brought in, water pumping stations were rehabilitated with new pumps, and electrical and compressed-air systems were upgraded.
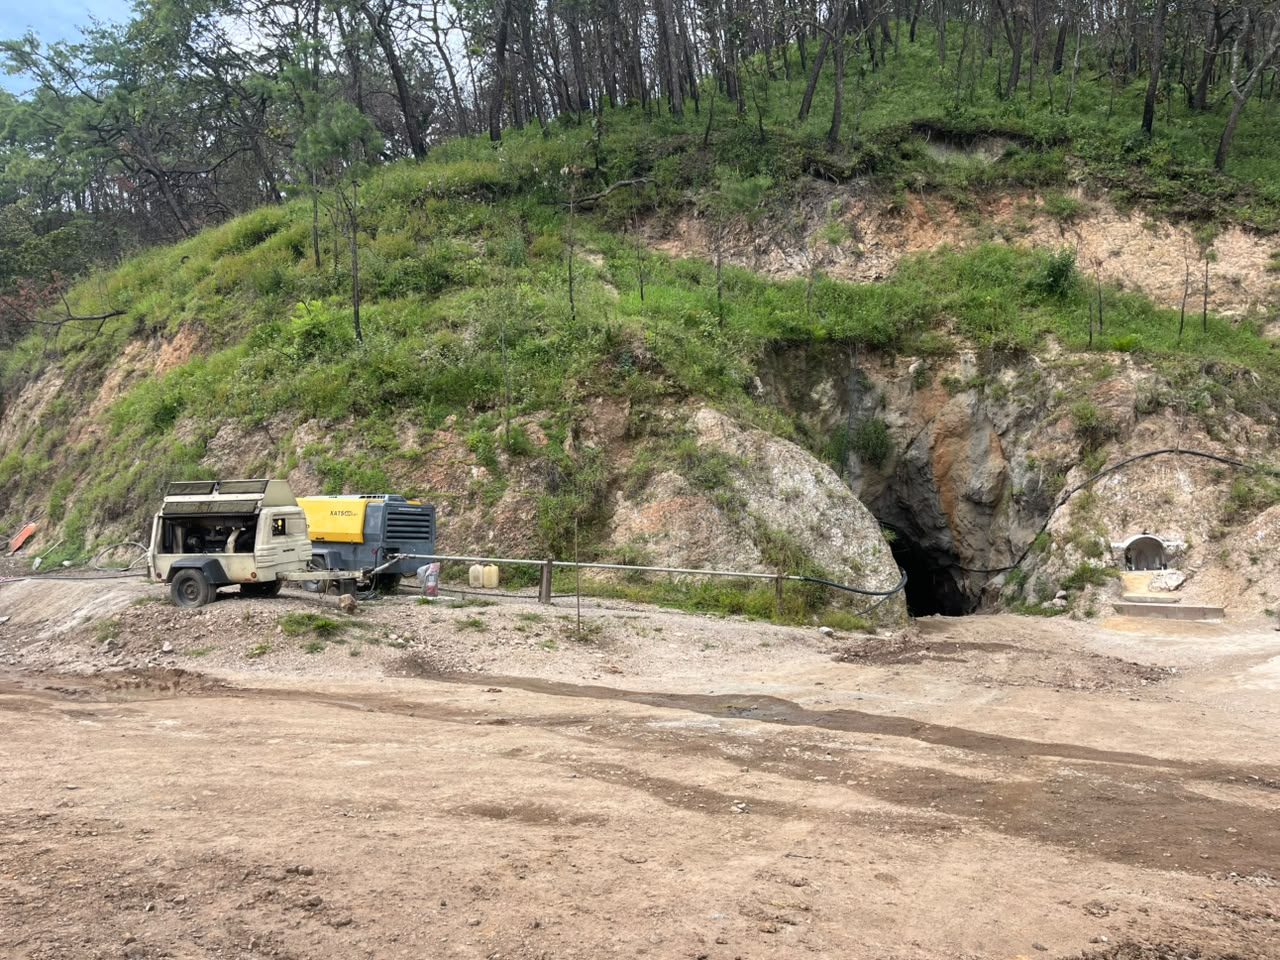
New mucking and hauling equipment brought into the mine.
Mine water pumping stations rehabilitated, including cleaning of sump 018.
New pumps installed, including a 40 HP pump at sump 018.
Mine electrical systems upgraded.
Mine compressed-air systems upgraded.
02Plant
The plant revamp added a 6′ × 6′ ball mill, a centrifugal decanter, a new electrical substation, an expanded tailings filtering station, new stainless-steel process tanks and revamped crushing circuits, alongside repairs and rehabilitation across the circuit.
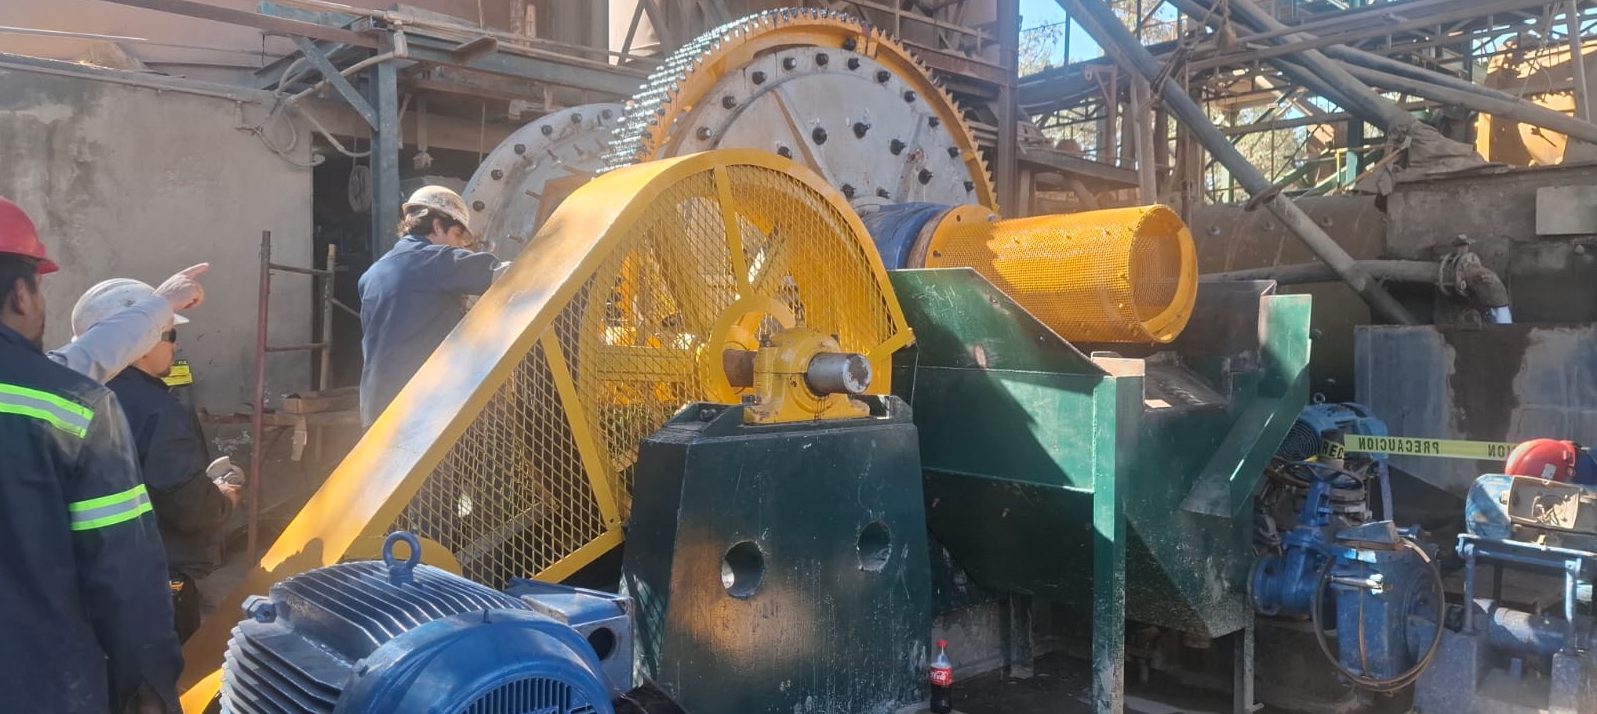
After the 6′ × 5′ mill went out of service in October 2025, the company sourced a used 6′ × 6′ mill, rebuilt and installed it, with a corresponding slurry pump upgrade. It was commissioned and began operating in late December 2025.
A high-speed centrifugal decanter for liquid-solid separation, installed and started up, recovers water, residual values and cyanide for reuse.
Water is recovered by the centrifugal decanter for reuse.
Cyanide is recovered for reuse, cutting fresh reagent consumption.
A new electrical substation, with a 750 kVA transformer and compact substation installed.
An expanded tailings filtering station, enabling dry-stacked tailings storage.
Tailings stored dry-stacked, rather than wet.
New stainless-steel process tanks, including two reagent tanks with stainless-steel piping and pumps, an acidity/basicity control tank, and a new 18,500-litre stainless-steel tank for ammonium bisulfite.
Primary, secondary and tertiary crushing circuits revamped, including repairs to the jaw crusher and the 4 ft and 3 ft cone crushers.
Existing drum filters fully rehabilitated. On vacuum filter no. 2, damaged steel was replaced, filter screens changed and the filter drive rebuilt.
Babbitt bearing replaced on the 6′ × 12′ ball mill.
Two new Butters filters constructed for the precipitation circuit.
A micro-balance for weighing gold and silver installed and in operation.
Tailings management
An expanded tailings filtering station allows tailings to be stored dry-stacked rather than wet. The company notes that this reduces the operation’s environmental footprint.
A centrifugal decanter recovers water, residual values and cyanide for reuse, which cuts fresh reagent consumption.